
Ceramic cutting tools can substantially increase material removal rates in heat-resistant superalloys and cast irons. However, they work effectively only within their intended operating window. Many trials fail because machining teams apply familiar carbide rules. This often includes reducing cutting speed when conditions become challenging. For carbide tools, lowering speed can be a sensible response to rapid wear, instability or edge failure. Higher temperatures can accelerate wear and shorten tool life. This experience strongly influences initial ceramic insert trials.
When the recommended cutting speed rises from 250 m/min to 900 m/min, the setting can seem unnecessarily aggressive. Operators may therefore begin at a much lower value. They expect this to create a safer and more controlled process. This cautious approach can prevent the ceramic tool from reaching its intended operating conditions. The result may be high cutting forces, poor wear behaviour and disappointing productivity. The ceramic grade is then often blamed. However, the actual cause may be operating outside its effective performance range. Ceramic machining is not simply a faster version of carbide machining. It relies on a different relationship between heat, material behaviour and cutting-edge performance.
Heat supports ceramic cutting
In high-speed machining of nickel-based superalloys and cast irons, heat does not always have the same negative effect as in conventional carbide machining. Nickel-based alloys have high strength at room temperature. As a result, deformation is difficult. As the cutting-zone temperature rises, the material begins to soften. Around 800°C, its resistance to deformation decreases significantly. Ceramic cutting materials retain hardness and wear resistance at temperatures that rapidly affect conventional carbide grades. This combination changes the cutting process. As temperature rises, the workpiece material becomes easier to cut. At the same time, the ceramic edge continues to withstand the load. Cutting forces can therefore decrease, while higher material removal rates become possible. High recommended cutting speeds have a functional purpose. They do not simply make the process faster. They generate the thermal conditions that support workpiece softening.
These conditions also allow the ceramic grade to operate effectively. A rough milling operation on Inconel 718 illustrates this effect. Increasing cutting speed from approximately 400 m/min to more than 1,000 m/min significantly reduced machining time. It also resulted in lower wear than the slower cutting conditions. For teams moving from carbide to ceramics, these results can seem counterintuitive. However, they reflect the operating principles of ceramic cutting materials.
Process stability remains essential
Higher speed alone does not ensure a successful ceramic machining process. Ceramics require stable conditions because the cutting edge must be protected from excessive impact loading and vibration. Rigid workholding, secure toolholding and minimal tool overhang are essential. In milling, smooth tool paths and fewer interruptions help reduce impact loads on the cutting edge. Stable engagement is equally important in turning. Consistent cutting conditions allow ceramic grades to operate within their intended range. When problems occur, improving setup stability is often more effective than immediately reducing cutting speed.
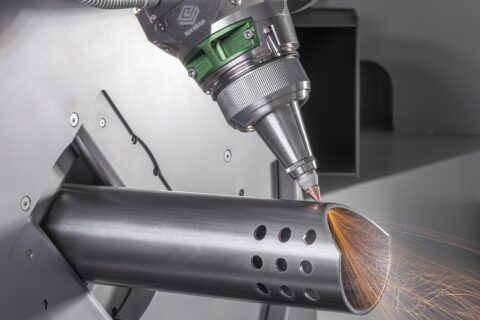
Coolant strategy also depends on the operation. Ceramic milling is typically performed dry because a high cutting temperature is part of the process. Intermittent coolant can create thermal shock through repeated heating and cooling of the cutting edge. This may damage the insert. In turning, coolant can often be used successfully. The cutting edge remains continuously engaged and does not experience the same repeated thermal cycles. The main adjustment for users is therefore both technical and operational. Ceramic inserts should not be treated as another carbide grade. Their performance depends on accepting higher cutting speeds and maintaining a rigid setup. Moreover, cutting conditions must support stable heat generation rather than attempting to prevent it.